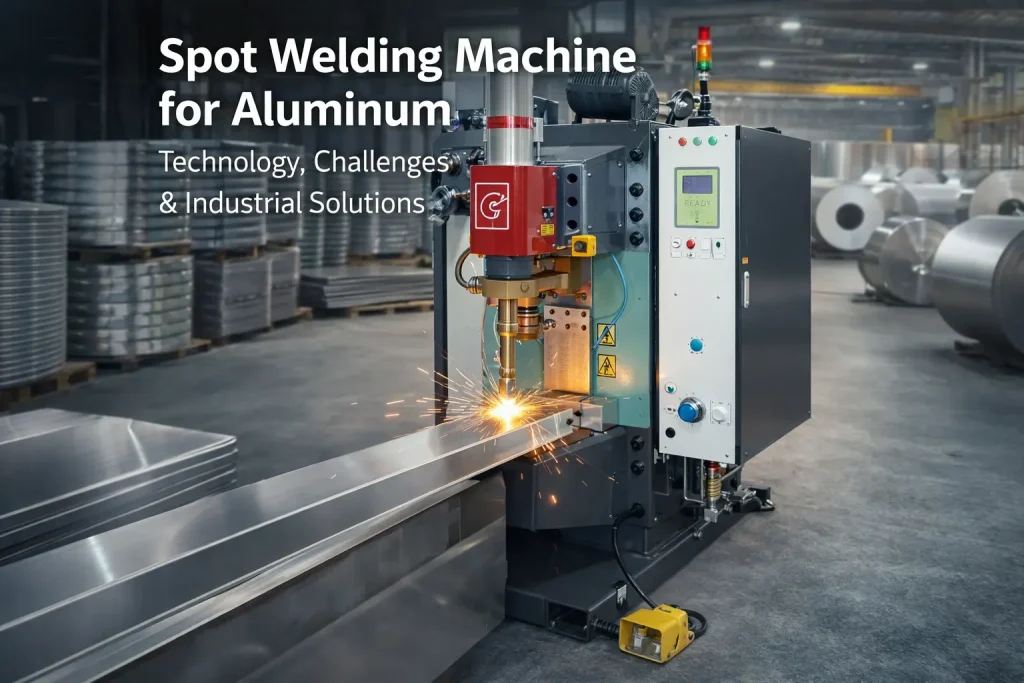
Silver contact spot welding machines are essential for producing electrical contacts in relays, circuit breakers, and precision electronic components. Due to silver’s high conductivity and thermal sensitivity, consistent weld quality requires precise control of process parameters and equipment configuration. This article covers key technical considerations for reliable welding performance.
I. Electrode Design and Material Selection:
1. Electrode Material Requirements
In silver contact spot welding machines, electrode performance directly impacts weld consistency and service life. Electrode materials must combine high electrical conductivity, strong resistance to wear and deformation, and excellent anti-adhesion properties. Common choices include CrZrCu (chromium zirconium copper) alloys, with hardness above HRB 80 and conductivity ≥80% IACS.
For high-temperature applications, dispersion-strengthened copper (Cu-Al₂O₃) is recommended, as it maintains mechanical strength and resists softening even at elevated temperatures.
2. Electrode Maintenance Strategy
Silver adhesion is a common issue in silver contact spot welding machines, causing unstable current distribution. Regular maintenance,including mechanical dressing or electrolytic polishing is required. Automatic electrode dressing is recommended every 500–1000 welds.

II. Welding Parameter Optimization:
1. Welding Current
Determine current based on the silver contact diameter, thickness, and base material properties. Typical current ranges from 3,000 A to 20,000 A. MFDC inverter welders provide stable current, reducing peak fluctuations.
2. Welding Pressure
Typical pressure ranges from 200 N to 1,000 N for stable contact resistance. Insufficient pressure may cause spatter or weak welds; excessive pressure may flattens contacts, deforms substrates, or damages tooling.
3. Welding Time
Time range is usually controlled between 5 ms and 200 ms, inversely related to current. Modern silver contact spot welding machines support multi-pulse modes (preheating, main welding, tempering) to improve nugget formation and reduce thermal stress.
4. Hold Time and Off Time
Hold time: Maintains pressure post-welding for nugget solidification.
Off time: Allows for electrode cooling and part replacement, affecting cycle time and heat dissipation.
5. Electrode Cooling
A closed-loop water cooling system is recommended, maintaining water temperature between 20-30℃ to prevent overheating, deformation, and accelerated electrode wear.
III. Industrial Applications of Silver Contact Spot Welding Machine
1. Relays and Contactors
- This is the most common application for silver contact spot welding machine. Current density should be ≥10⁴ A/cm²to ensure sufficient penetration in small contact areas.
- With the help of a vision positioning system, the silver dot and the electrode are precisely aligned, with alignment accuracy within ±0.05 mm.
- Common materials include AgNi and AgSnO₂ contacts welded to copper strips or Fe-Ni alloy springs.

2. Circuit Breaker Contact Welding
- For high current applications (≥100A), weld joints must provide high current carrying capacity and resistance to electrodynamic forces.
- We recommend using MFDCinverter resistance welding machine, as its DC output characteristics reduces inductive reactance effects, improves energy efficiency, and offers better output stability compared to AC welder
- Electrodes are typically made of tungsten-copper composites or copper alloys with tungsten blocks to enhance wear resistance and anti-sticking performance.
3. Microelectronic and Sensor Welding
- In micro-switches, MEMS devices,and precision sensors, silver contact diameters can be under 2 mm. Welding force must be precisely controlled within 10-100N.
- Advanced silver contact spot welding machines use servo-driven systems with force-displacement-time closed-loop control, enabling multi-dimensional control to prevent damage to sensitive components.
- Typical applications include welding silver contactsto dissimilar material combinations such as ceramic substrates and gold-plated lead frames.
IV. Common Welding Defectsand Solutions
1. Lack of Fusion
- Causes: Insufficient current or weld time, surface contamination, electrode wear.
- Solutions: Increase welding current or extend welding time; clean the surface of welding parts; replace or re-grind the electrodes; use a real-timewelding monitoring system to collect dynamic resistance curves and evaluate nugget formation.
2. Cracking
- Causes: Excessive heat input, slow cooling, or material
- Solution: Use pulse welding to control heating and cooling stages; optimize electrode cooling water flow.
3. Misalignment or Deformation
- Causes: Poor electrode alignment, uneven pressure, or loose fixtures.
- Solution: Calibrate electrode concentricity; improve fixture design; introduce force sensors for real-time monitoring.
A high-performance silver contact spot welding machine is critical for ensuring reliable, low-resistance electrical connections in modern industrial applications.
By combining optimized electrode materials, precise parameter control, advanced MFDC technology, and real-time quality monitoring, manufacturers can achieve high-strength, low-resistance, and highly reliable connections between silver contacts and base materials, ensuring long-term stable operation in power systems, industrial control, and automotive electronics.