Introduction
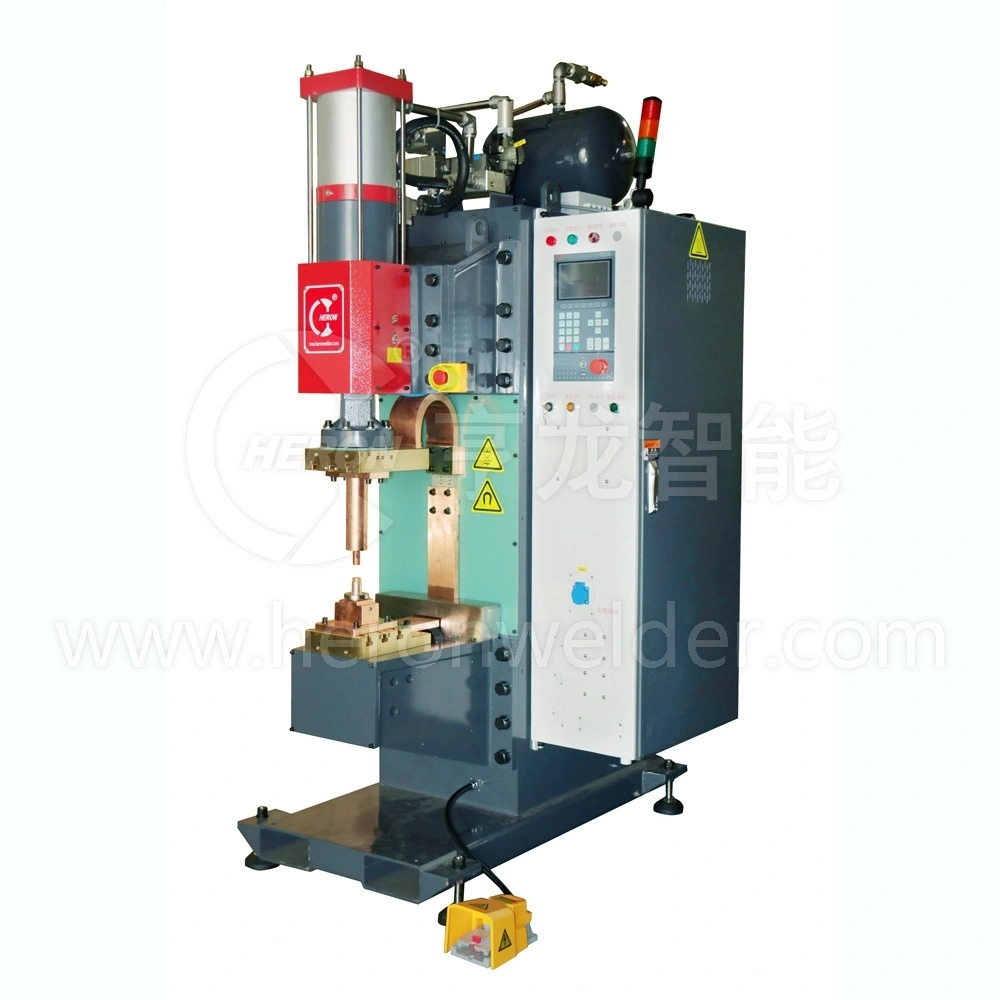
Spot welding problems such as burn-through, weak welds, welding spatter, distortion, indentation, and cracking can affect weld quality, part appearance, and production consistency. Understanding the causes behind these issues helps manufacturers adjust welding parameters, electrode conditions, and part positioning for more stable results. For demanding welding applications, choosing suitable spot welding equipment is also important for maintaining consistent weld quality.

1. Burn-Through
Burn-through occurs when the weld nugget grows excessively and penetrates completely through the sheet, leaving a hole in the part.
Causes
- Welding current is too high
- Electrode force is too low
- Contamination on the sheet surface
- Poor cooling performance
- Uneven or contaminated electrode faces
- Welding time is too long
Corrective Measures
- Dress the electrodes and increase the electrode contact area as appropriate
- Reduce the welding current
- Increase electrode force as appropriate
- Check the temperature of the main welding cables
- Reduce welding time as appropriate
Proper control of welding current, electrode force, and welding time is essential for preventing spot welding problems such as burn-through.
2. Weak Weld
A weak weld occurs when no effective weld nugget forms, or when the nugget is too small to meet the required load capacity. It is one of the most common spot welding problems in production.
Causes
- Welding time is too short
- Electrode force is too high
- Welding current is too low
- Electrode face area is too small or too large
- Poor cooling performance
- Poor fit-up between parts
- Weld points are too close to each other
- Weld point is too close to the sheet edge
- Poor weldability of the material
- Electrode angle is not perpendicular to the part
Corrective Measures
- Re-adjust the relationship between welding current and welding time
- Re-adjust electrode force
- Use electrodes with a suitable face area
- Add external cooling equipment where necessary
- Adjust weld point spacing and position
- Use a material with better weldability
- Correct the welding angle
3. Burr and Welding Spatter
Welding spatter occurs when molten metal is expelled from the welding zone and adheres to the sheet surface after solidification, forming burrs. Spatter can occur internally or externally, with excessive contact resistance being a primary cause. Excessive spatter is often linked to unstable welding conditions, making it an important factor when diagnosing spot welding problems.
Factors Affecting Internal Spatter
- Pre-squeeze time is too short
- Electrode force is too low
- Contamination on the sheet surface
- Poor fit-up between parts
- Weld point is too close to the sheet edge
- Electrode angle is not perpendicular to the part
- Welding current is too high
- Poor electrode alignment
- Poor weldability of the material
Factors Affecting External Spatter
- Pre-squeeze time is too short
- Welding time is too long
- Hold time is too short
- Electrode force is too low
- Insufficient cooling
- Contamination on the sheet surface
- Poor fit-up between parts
- Electrode angle is not perpendicular to the part
- Electrodes have been used for too long
- Welding current is too high
- Poor electrode alignment
- Poor weldability of the material
Corrective Measures
- Clean the sheet surface
- Adjust the weld point position
- Correct the welding angle
- Increase pre-squeeze time as appropriate
- Increase electrode force as appropriate
- Reduce the welding current as appropriate
4. Weld Point Distortion
Weld point distortion occurs when the sheet surface deforms around the weld point. A weld point is considered unacceptable when the distortion angle exceeds 25°.
Causes
- Poor electrode alignment
- Electrode angle is not perpendicular to the part
- Welding gun movement before the end of the welding cycle
Corrective Measures
- Align the electrodes properly
- Correct the welding angle
- Prevent welding gun movement before the welding cycle is complete
Proper electrode alignment is particularly important when troubleshooting spot welding problems related to weld point appearance and dimensional consistency.
5. Excessive Indentation
Excessive indentation is a visible result of excessive plastic deformation of the sheet. A weld point is considered unacceptable when the indentation depth exceeds 50% of the sheet thickness on either sheet.
Causes
- Welding time is too long
- Electrodes have been used for too long
- Pre-squeeze time is too short
- Electrode force is too low or too high
- Welding current is too high
- Electrode face area is too small
- Insufficient cooling
- Poor weldability of the material
- Electrode angle is not perpendicular to the part
Corrective Measures
- Dress the electrodes
- Increase the electrode contact area as appropriate
- Adjust the welding parameters as appropriate
6. Cracking
Cracking can occur when excessive internal stress develops in or around the weld during cooling. It is another critical issue when evaluating spot welding problems, particularly when welding conditions cause excessive thermal stress.
Causes
- Different coefficients of thermal expansion between dissimilar base metals can generate excessive internal stress during cooling
- Uneven heating of the same material can cause non-uniform shrinkage during cooling
- Relative movement between the parts while the weld is solidifying
- A wide solidification temperature range
- Excessive weld brittleness
In simple terms, cracking is caused by thermal expansion and contraction. The weld area expands when heated, and excessive internal stress during cooling can cause the weld nugget to crack.
Corrective Measures
- Appropriately increase hold time
- Add or extend post-heating
- Apply a tempering cycle where required
- Use a slower current decay rate
- Use a slower current rise rate
7. Electrode Force
Electrode force directly affects heat generation and plastic deformation in the welding zone. As electrode force increases, contact resistance decreases and current density is reduced, slowing the rate of heat generation and reducing weld nugget diameter. As a result, weld strength generally decreases as electrode force increases. When electrode force is increased, welding time or welding current may need to be adjusted appropriately to enlarge the weld nugget and improve weld strength. If electrode force is too low, excessive spatter may occur, which can also reduce weld strength. For this reason, electrode force should be considered together with welding current, welding time, electrode condition, and material weldability when addressing spot welding problems.
Conclusion
Most spot welding problems are related to the interaction between welding current, welding time, electrode force, electrode condition, cooling, material properties, and part positioning. Identifying the specific defect first, then checking the relevant welding parameters and electrode conditions, provides a practical starting point for troubleshooting. Consistent electrode maintenance, accurate alignment, proper cooling, and appropriate welding parameters are essential for stable weld quality and repeatable production.