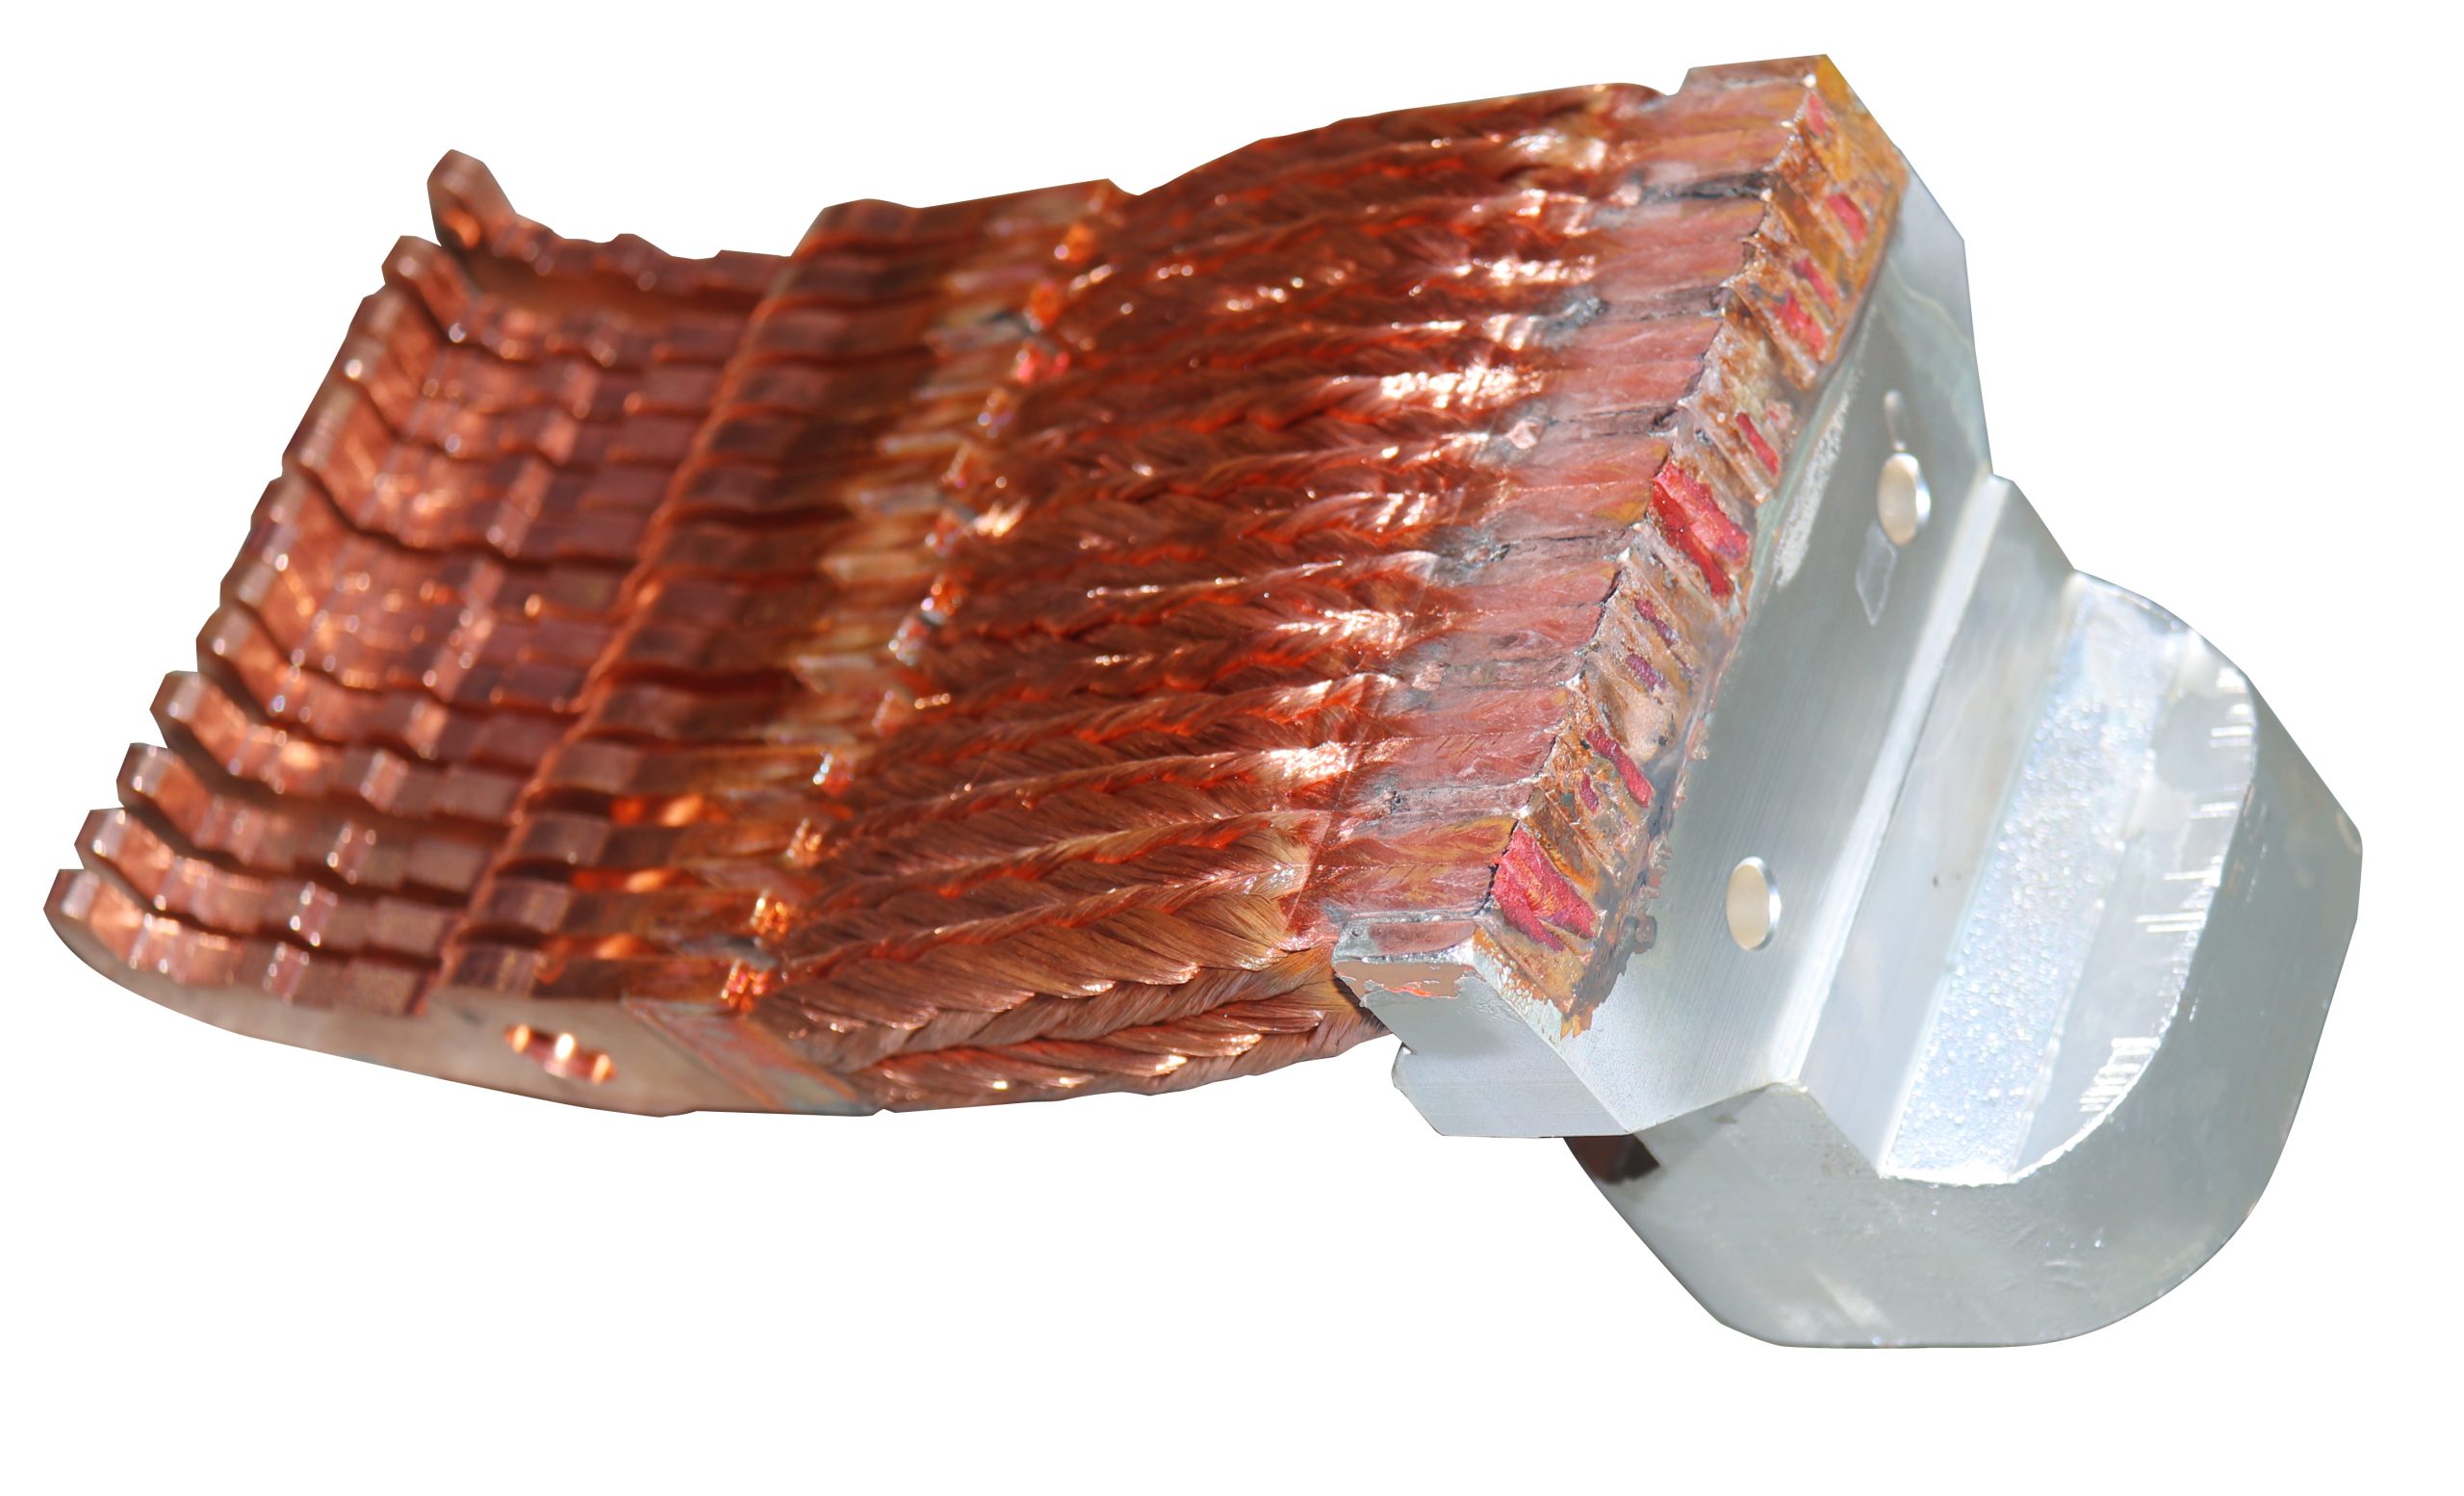
Busbar Welding Machine | MFDC Welder For Frame Breaker DB-2000-24001

Specifications

Model # DB-440-22022
Rated Capacity KVA 440
Power Supply V/Φ/HZ 380/3/50
Max. Primary Current A 250
Max. Short Cut Current KA 40
Max. Working Pressure KN 0.1
Dimension(LxWxH) mm 1901x1127x2226
 

01

High-Power MFDC Welding Technology

Rated at 2000KVA with a maximum output current of 40KA at 100% duty cycle, the MFDC welder uses TI DSP control with 16-bit current regulation for high-current copper welding. Constant current, duty cycle, and hybrid power modes provide precise current control, controlled penetration, and stable weld strength for copper busbar assemblies.

02

Automated Positioning & Clamping System

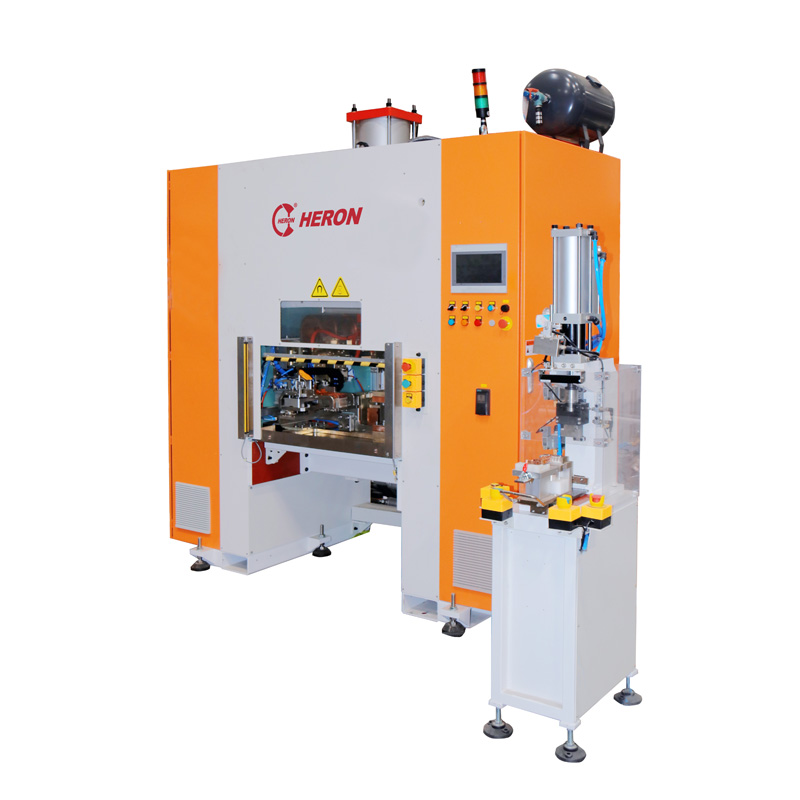
A three-axis transfer mechanism, dual-piston cylinder, and dedicated pressing station enable automatic part positioning and weld point switching. The 250mm large-bore cylinder provides up to 49KN electrode force, while vision inspection verifies part orientation and soft connection position before welding.

03

Penetration & Cooling Control System

Part height and thickness are monitored before welding to detect loading deviations and dimensional changes. Closed-loop penetration control stops current output when the preset depth is reached. Independent cooling units for transformer and electrodes, combined with multi-channel water flow and temperature monitoring, maintain stable thermal conditions.

04

PLC Control & Data Traceability

Siemens PLC and Kunlun Tech HMI provide welding program management, parameter control, and user access management. Welding current, time, pressure, penetration depth, waveform data, and alarm records are stored for process tracking, USB export, and remote diagnostics.

05

Safety Interlock Protection System

The enclosed safety cabin isolates welding spatter and arc radiation. Safety light curtains, door interlocks, electrical cabinet switches, emergency stops, and status indicators monitor operating conditions. Welding operation is disabled when safety requirements are not met.

06

Dual-Station Production Layout

The dual-station layout separates preparation and welding operations, allowing loading, clamping, and vision inspection before welding. Parallel station operation reduces preparation impact on cycle time, achieving 60–80 seconds per part with storage racks and material carts for continuous production.

Get in touch with us

Whether you are looking for a quotation or partnership support, we are happy to assist you.

Scroll to Top
Free Quote & Information Request